
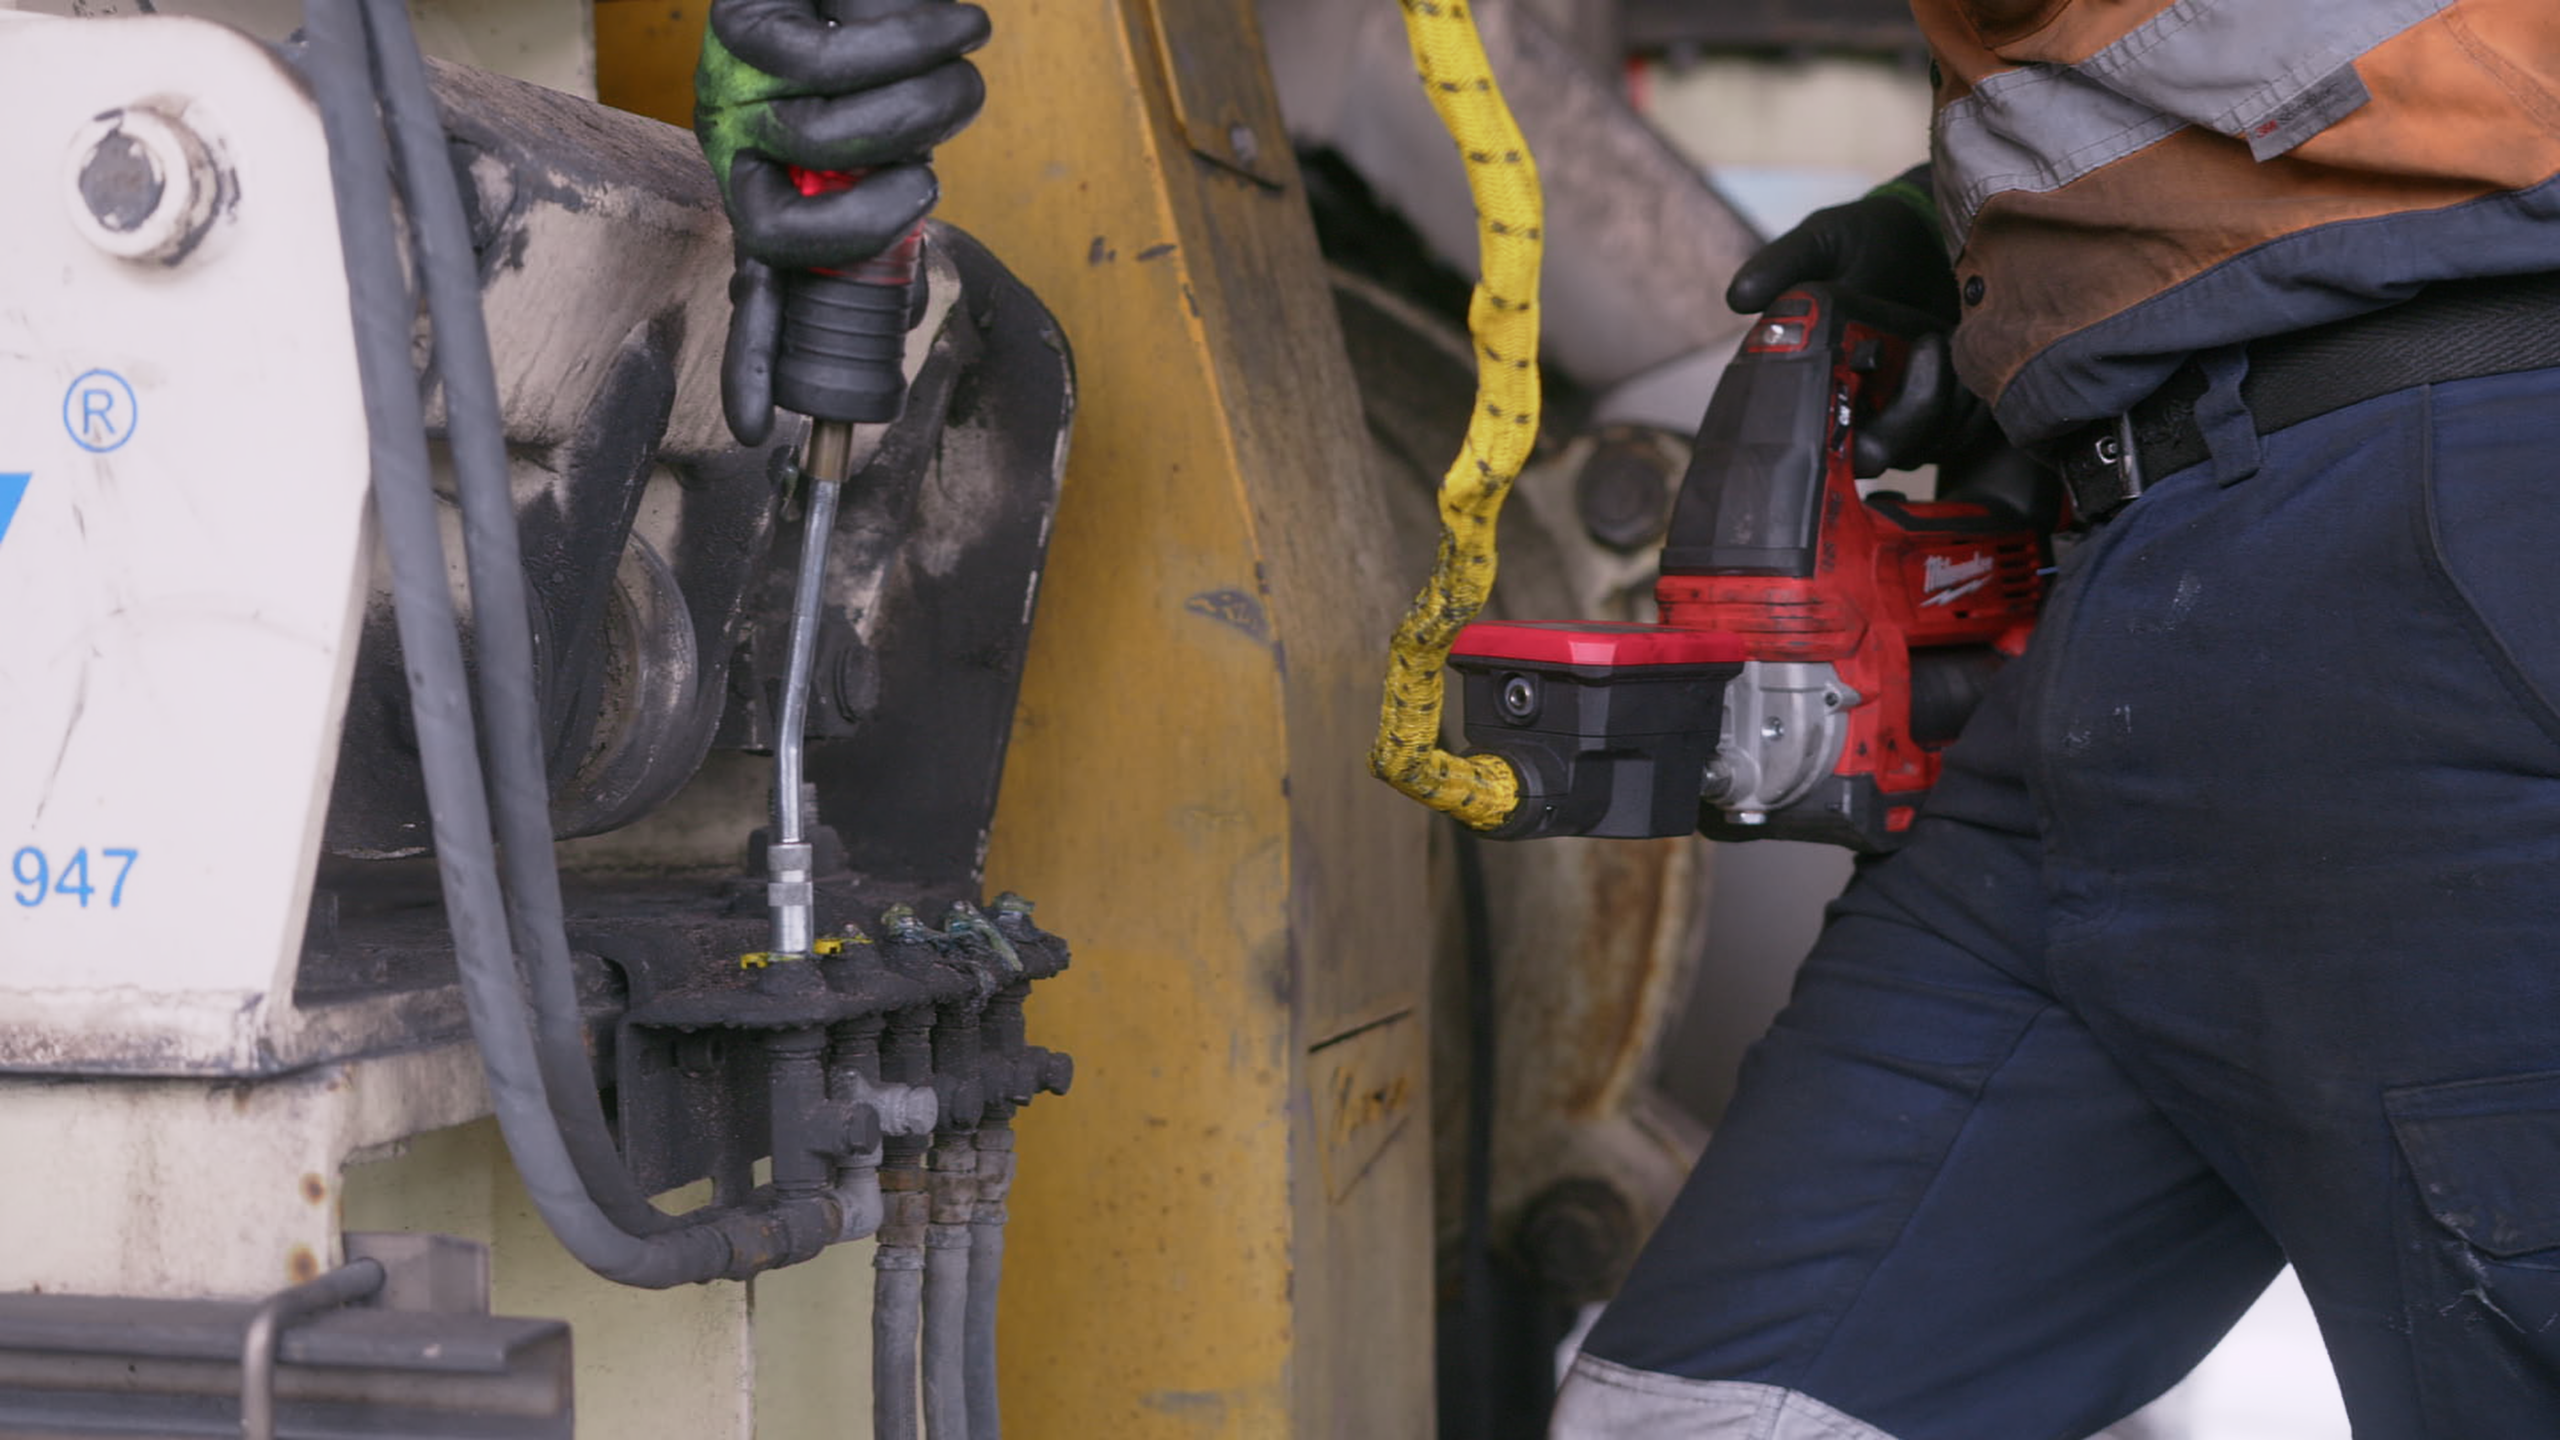
Planned vs Actual Greasing
Planned greasing defines which lubrication points need attention, when they need it, and how much grease to apply. Actual greasing records what was done, including incomplete work and exceptions. Comparing the two gives maintenance teams a practical way to assess manual greasing compliance without confusing a closed work order with verified lubrication.
The goal is not simply to finish more routes. It is to make the work traceable enough to identify gaps, investigate deviations, and improve the next maintenance decision.
What is the difference between planned and actual greasing?
Planned greasing is the approved instruction for a lubrication task; actual greasing is the recorded execution of that instruction. A useful comparison connects the same lubrication point, lubricant, quantity, and timing on both sides. SKF’s lubrication management guidance calls for task histories that show what was performed, when, and under what conditions, alongside sufficiently detailed instructions. (skf.com)
Consider a hypothetical conveyor route. The plan lists each grease point individually, but the work order only asks whether the conveyor was lubricated. If one fitting cannot be reached, marking the whole machine complete leaves no visible distinction between finished work and an unresolved exception.
Instead, structure the comparison at point level:
| Record | Planned information | Actual information |
|---|---|---|
| Identity | Asset and lubrication point | Point serviced or exception recorded |
| Timing | Due date or operating-hour trigger | Completion date and relevant hours |
| Lubricant | Approved grease identification | Grease used |
| Quantity | Specified amount and units | Recorded amount and measurement method |
| Status | Required task and procedure | Complete, partial, blocked, or deferred |
Treat this as a suggested record design, not a requirement to buy software. A controlled paper sheet can use the same fields as a digital route.
Build a lubrication schedule that technicians can execute
Before judging execution, check whether the plan is technically sound and clear enough to follow. Relubrication quantity and frequency both matter, and the appropriate interval depends on application conditions. SKF identifies temperature, speed, and environment as relevant to routine greasing frequency, while bearing size influences quantity. (cdn.skfmediahub.skf.com)
Use manufacturer guidance as the starting point for the lubrication schedule, then have qualified personnel review application-specific requirements. Do not turn one machine’s instruction into a plant-wide default. Where information is missing, flag it for review rather than filling the gap with an assumed number of grease-gun strokes.
For each task, aim to provide:
- An unmistakable location: Identify the component and individual point, supported by a labeled photograph where useful.
- A clear lubricant reference: Specify the approved product or controlled specification rather than an informal description.
- An actionable quantity: State the amount and units, plus the approved method for delivering it.
- An explicit trigger: Distinguish calendar-based work from operating-hour requirements.
- A usable procedure: Include access arrangements, applicable safety instructions, and what to do when the task cannot be completed.
Walk through the draft route with a technician before releasing it. Ask them to locate every point and explain each instruction. Resolve ambiguous labels or missing access information before those uncertainties become execution disputes.

Missed grease points need visible exception handling
Design the workflow so technicians can report missed grease points honestly. An inaccessible fitting should not require a choice between falsely completing the task and leaving an unexplained blank. Provide distinct statuses for attempted, partially completed, deferred, and not attempted work.
Ask for a short reason whenever the actual result differs from the plan. Useful categories might include access unavailable, equipment unavailable, fitting problem, lubricant unavailable, or instruction unclear. Add free text for details that a category cannot capture.
For example, “access unavailable—guard removal requires planned intervention” gives the planner something concrete to resolve. “Not done” does not explain the next action. These are suggested reporting conventions; adapt them to the site’s maintenance and safety procedures.
Give each unresolved exception an owner and a follow-up decision. Decide whether it requires a revised access arrangement, repair work, technical review, or rescheduling. Keep that decision separate from the original completion record so the history remains understandable.
Over greasing and undergreasing are both deviations
Applying more grease is not automatically better maintenance. Excessive quantities can cause churning and overheating, particularly at high speeds, while insufficient lubrication can also harm bearing performance. Both over greasing and undergreasing belong in the planned-versus-actual review—not just missed visits. (cdn.skfmediahub.skf.com)
Record quantity deviations without treating every difference as technician error. First check whether the specified amount, units, delivery method, and procedure were understood. Then investigate whether the equipment or application requires technical attention.
Where quantity verification is important, consider an appropriate grease meter rather than relying solely on an unmeasured application. Such meters measure grease dispensed from the gun, providing a quantity record for comparison with the planned amount. (tricocorp.com)
Keep the interpretation narrow: a recorded dispensing quantity is evidence about dispensing. It should not be presented as a complete assessment of bearing lubrication. SKF identifies blocked piping, incorrect assembly, and bearing arrangement problems among the reasons lubricant may not reach a bearing. (skf.com)
If a task is overdue, do not invent a catch-up dose. Refer the situation to the approved procedure or a qualified reviewer rather than assuming that doubling the next application will restore the intended condition.
How can lubrication verification go beyond a completion tick?
Lubrication verification should compare task evidence with the approved instruction and preserve any unresolved uncertainty. A completion tick records a reported status; a stronger record also identifies the point, timing, lubricant, quantity, and exceptions. This approach follows the distinction in SKF’s guidance between detailed task instructions and retrievable execution history. (skf.com)
For your own workflow, separate three questions: Was the correct point identified? Was the specified work performed and recorded? Is further investigation needed before the result can be accepted? Keeping these questions separate avoids asking one checkbox to represent several different judgments.
A practical review checklist is:
- Match the point. Confirm that the record refers to the intended component, not merely the parent machine.
- Compare timing. Identify late completion and distinguish it from work still outstanding.
- Review quantity evidence. Compare like units and note whether the amount was measured or estimated.
- Read the exception. Check whether partial work or an access problem needs follow-up.
- Assign the next action. Accept the record, request clarification, or open corrective work.
Apply review effort according to the site’s priorities. You might begin with critical assets, repeat exceptions, or routes with unclear records. Present this as a review strategy, not proof that unreviewed tasks were completed correctly.
Measure compliance without hiding the gaps
Define manual greasing compliance before putting a percentage on a dashboard. For a proposed point-level measure, divide tasks completed within the approved window by tasks due in that period. State the rules beside the result, including how partial tasks, canceled work, and approved deferrals are treated.
Keep completion and verification visible separately. A reported-complete task may still need clarification, while a properly documented exception may demonstrate good reporting even though the physical work remains unfinished. Avoid rewarding a clean-looking dashboard at the expense of accurate records.
Consider tracking:
- On-time point completion: Due tasks reported complete within the defined window.
- Open exceptions: Unresolved tasks, grouped by reason and age.
- Quantity deviations: Records outside approved application requirements.
- Evidence completeness: Records containing the fields required for review.
Use these measures together rather than combining them into a score that conceals the underlying issues. Review patterns with technicians and planners before drawing conclusions about individual performance.
Turn the comparison into better bearing reliability decisions
Use the review meeting to resolve causes, not simply repeat the overdue list. Select recurring exceptions, agree on the next action, and check at the following review whether that action was completed. If a task instruction changes, preserve the previous version so historical comparisons remain meaningful.
Treat bearing reliability as the objective, not a benefit proven by higher completion alone. Correct lubricant selection, application quantity, timing, and delivery all matter; a compliance report addresses only part of that picture. (skf.com)
Start with one manageable route. Confirm its points, clarify its instructions, and record actual work consistently. The most useful planned-versus-actual comparison is one that helps the team decide what needs attention next—not one that merely makes the schedule look finished.